
 techsales@metzix.com
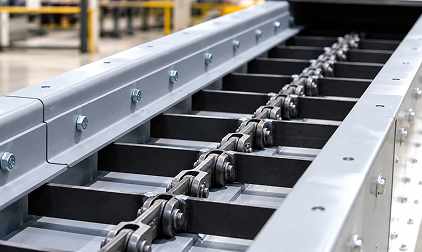
Chain Conveyors
Industrial Grade • Heavy Duty
“
Reliable transport for heavy-duty materials in abrasive environments.
Engineering Overview
Chain conveyors are designed for reliable transport of bulk materials in demanding industrial and mining applications.
Typical systems handle capacities from 1 to 1,000+ t/h and are suitable for conveying distances from 10 to 200 m, depending on material characteristics and system configuration.
Benefits
| Benefit | Description |
|---|---|
| Robust design | Robust design for heavy-duty materials. |
| Abrasive environments | Reliable operation in abrasive environments. |
| Inclined and enclosed | Suitable for inclined and enclosed conveying. |
| Low maintenance | Low maintenance and long service life. |